US12759038 - Method of manufacturing a high-pressure cartridge case
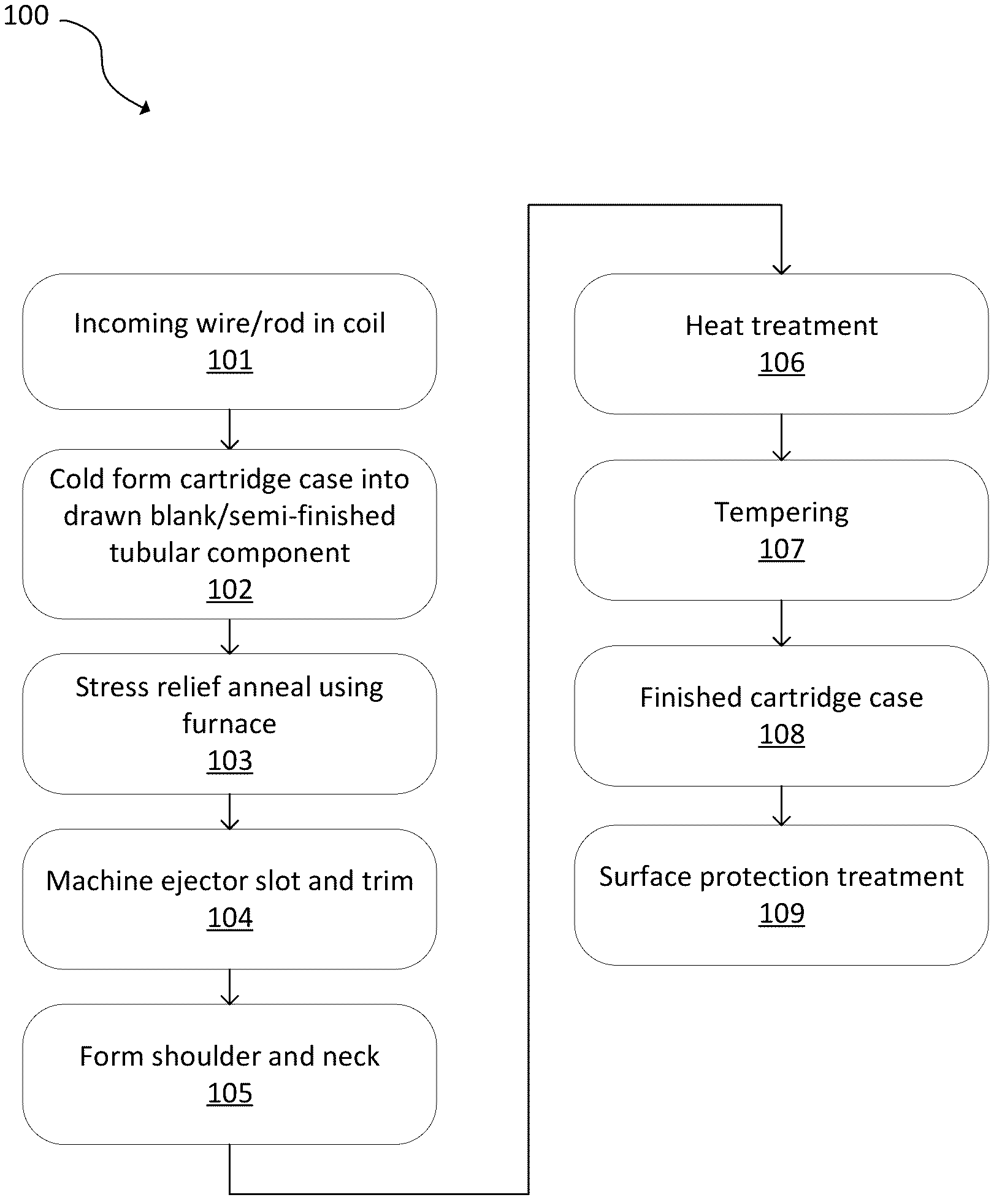
The patent describes a method for manufacturing high-pressure cartridge cases through a series of processes including cold forming, annealing, and heat treatment. It emphasizes the use of specific materials and techniques, such as spheroidized annealing and oil quenching, to enhance the properties of the cartridge case.
Claim 1
1 . A method comprising: providing a wire or rod; cold forming a cartridge case into a drawn blank or a tubular component from sheared lengths of the wire or rod; annealing the cartridge case using a belt furnace, flame furnace, induction furnace, or a batch furnace; performing a machine ejector slot and trim on the cartridge case; forming a shoulder and a neck of the cartridge case; performing a heat treatment of the cartridge case; and tempering the cartridge case; wherein one or more of the following: the wire or rod is spheroidized annealed at finished size (SAFS) before cold forming; after performing the heat treatment and before tempering the cartridge case, the method further comprises oil quenching the cartridge case; or the wire or rod comprises a precipitation-hardened copper alloy. providing a wire or rod; cold forming a cartridge case into a drawn blank or a tubular component from sheared lengths of the wire or rod; annealing the cartridge case using a belt furnace, flame furnace, induction furnace, or a batch furnace; performing a machine ejector slot and trim on the cartridge case; forming a shoulder and a neck of the cartridge case; performing a heat treatment of the cartridge case; and tempering the cartridge case; wherein one or more of the following: the wire or rod is spheroidized annealed at finished size (SAFS) before cold forming; after performing the heat treatment and before tempering the cartridge case, the method further comprises oil quenching the cartridge case; or the wire or rod comprises a precipitation-hardened copper alloy. the wire or rod is spheroidized annealed at finished size (SAFS) before cold forming; after performing the heat treatment and before tempering the cartridge case, the method further comprises oil quenching the cartridge case; or the wire or rod comprises a precipitation-hardened copper alloy.
Google Patents
https://patents.google.com/patent/US12759038
USPTO PDF
https://image-ppubs.uspto.gov/dirsearch-public/print/downloadPdf/12759038